09/08/2026
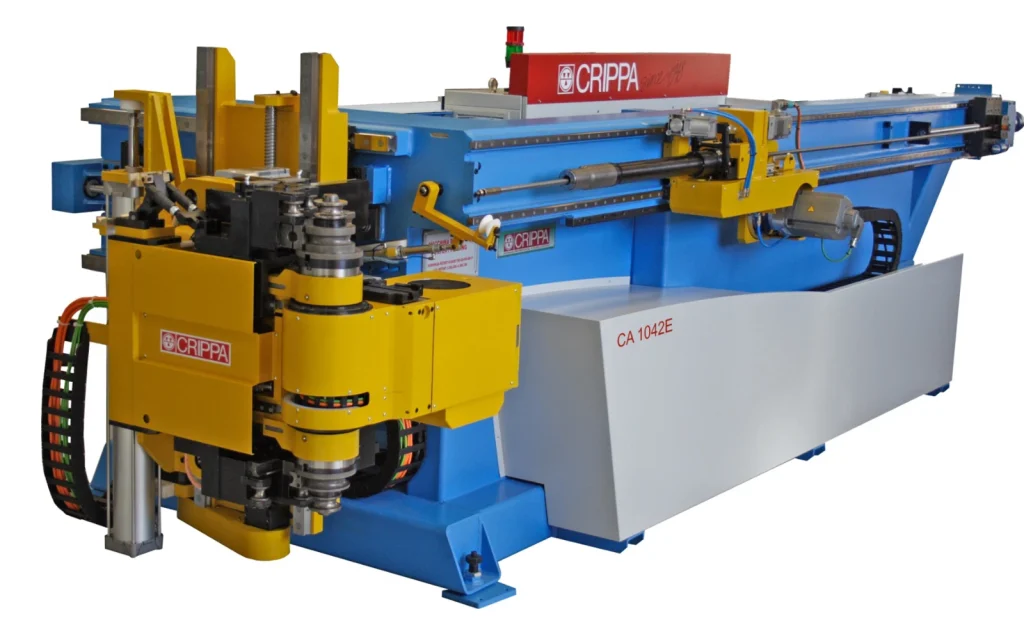
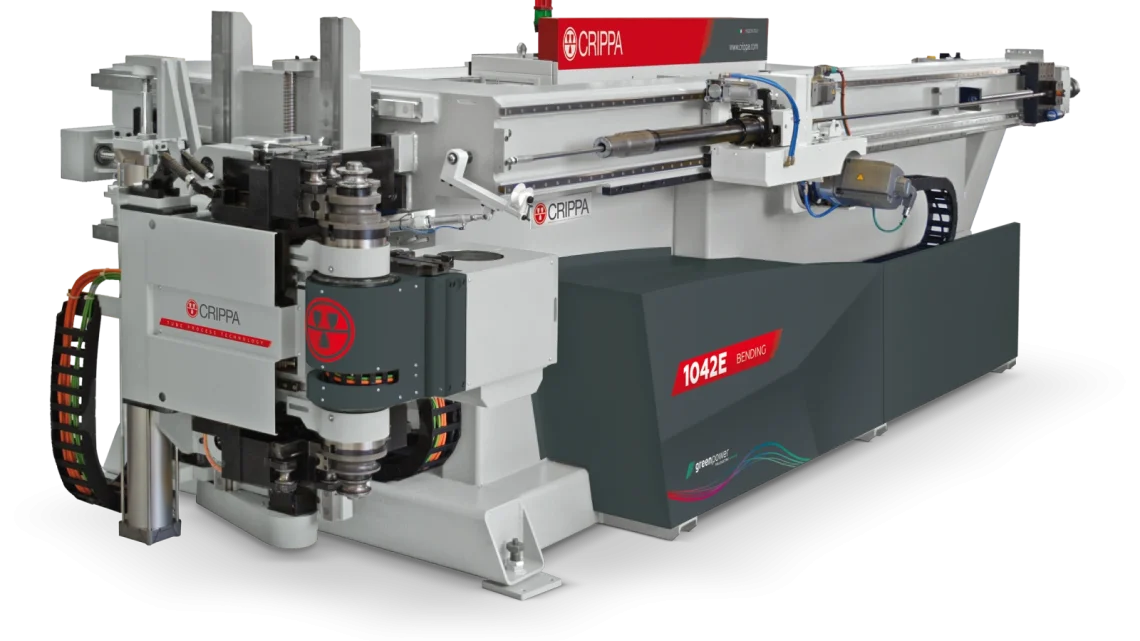
For Sale : used CRIPPA CA 1042E CNC 20kW Electric 10-Axis Right/Left Tube Bending Machine Max. Tube Ø 42mm – Year 2013 made in Italy
CRIPPA CA 1042E CNC 20-kW Fully Electric 10-Axis Right/Left Tube Bending Machine – Year 2013
-
Extremely low hours, less than 500 hours of total operation. Only used for prototyping- production never came to fruition.
CRIPPA CA 1042E Machine Catalogue INFORMATION |
||
|---|---|---|
| Specification | Metric | Imperial |
| Manufacturer | CRIPPA | |
| Model | CA 1042E | |
| Year | 2013 | |
| Machine Type | CNC Fully Electric Tube Bending Machine | |
| Series | UP&DOWN | |
| Bending Direction | Right and Left | |
| Number of CNC Axes | 10 | |
| Drive Technology | Fully Electric Digital Motors | |
| CNC Control | Siemens SINUMERIK 840D sl | |
| TUBE BENDING CAPACITY | ||
| Maximum Mild Steel Tube Capacity | Ø 42 × 2 mm | Ø 1.654″ × 0.079″ |
| Mild Steel Strength Range | R = 350–450 N/mm² | Approx. 50,763–65,267 psi |
| Maximum Stainless Steel Tube Capacity | Ø 42 × 1.3 mm | Ø 1.654″ × 0.051″ |
| Maximum Bending Radius | 150 mm | 5.906″ |
| Maximum Bending Speed | 240°/sec | 240°/sec |
| Maximum OD for Hitch Feeding | 37 mm | 1.457″ |
| CLR / DIA Capability | Capable of bending tubes with CLR/DIA ratio lower than 0.8 | |
| Variable Radius Bending | Capable of thrust bending with variable radius | |
| TUBE FEEDING & WORKING LENGTH | ||
| Standard Workable Tube Length Inside Collet / Hitch Feeding | 1,600 / 3,300 mm | 62.99″ / 129.92″ |
| Maximum OD for Hitch Feeding | 37 mm | 1.457″ |
| AXES & MOVEMENT | ||
| Number of CNC Axes | 10 | |
| Y-Axis Resolution | ± 0.05 mm | ± 0.002″ |
| Stroke | 145 mm | 5.709″ |
| Head Movement | Orthogonal Movement | |
| Head Positioning Capability | Above, Below, Right and Left of the Tube | |
| Working Plane Change | Automatic / Dynamic Working Plane Positioning | |
| MULTISTACK BENDING SYSTEM | ||
| Machine Configuration | Multistack Tube Bending Machine | |
| Working Planes | At Least 6 Working Planes | |
| Multiple Tool Capability | Multiple Tools with Different Radii and Clamping Configurations | |
| Right-Hand Bending | Yes | |
| Left-Hand Bending | Yes | |
| Right & Left Bending in One Machine | Yes | |
| CLAMPING & PRESSURE DIE SYSTEM | ||
| Clamp Die Operation | CNC Controlled / Synchronous | |
| Pressure Die Operation | CNC Controlled / Synchronous | |
| Synchronous Die Movement | When the Upper Plane Moves Forward, the Lower Plane Moves Back, and Vice Versa | |
| Clamp & Pressure Die Drive | High-Load Ball Screws | |
| Dynamic Plane Positioner | Included | |
| Collision Protection Function | Dynamic Plane Positioning Helps Limit Component Damage in Case of Accidental Collisions | |
| LINEAR MOTION SYSTEM | ||
| Linear Guides | Lubrication-Free Linear Guides | |
| Linear Carriages | Recirculating Ball Carriages | |
| Clamp / Pressure Die Transmission | High-Load Ball Screws | |
| CNC CONTROL & SOFTWARE | ||
| CNC Control System | Siemens SINUMERIK 840D sl | |
| Motor Technology | Fully Electric Digital Motors | |
| Operator Display | 19″ LCD Touch Screen | 19″ LCD Touch Screen |
| Graphical Software | Three-Dimensional Graphical Software | |
| User Interface | UII – User ISO Interface | |
| Programming Functions | Tube Bending Process Programming | |
| Simulation Functions | Bending Process Simulation | |
| Process Optimisation | Bending Process Optimisation via UII | |
| Smart Factory Compatibility | Designed for Integration into Smart Factory Systems | |
| AUTOMATION & PRODUCTION | ||
| Loading Cycle Integration | Supported | |
| Unloading Cycle Integration | Supported | |
| Work Cell Integration | Suitable for Integration into Automated Work Cells | |
| Single-Cycle Complex Bending | Designed to Produce Complex Tubes in a Single Cycle, Reducing the Need for Post-Processing Operations | |
| Working Plane Flexibility | Rapid Change Between Multiple Working Planes | |
| ELECTRICAL DATA | ||
| Installed Power | 20 kW | Approx. 26.8 HP |
| Voltage | 400 V | |
| Mains Frequency | 50 Hz | |
| Energy Efficiency | Fully Electric Drive Technology Designed for Reduced Energy Consumption | |
| Pneumatic Balancing | Included – Allows the Use of a Smaller, High-Performance Motor | |
| MACHINE WEIGHT | ||
| Machine Weight | 3,800 kg / 3.8 metric tons | Approx. 8,378 lbs / 4.19 US tons |
| KEY MACHINE FEATURES | ||
| Fully Electric Technology | 10 CNC Axes Driven by Fully Electric Digital Motors | |
| Bidirectional Bending | Right and Left Tube Bending Capability | |
| Orthogonal Head Movement | Head Can Move Above, Below, Right and Left Relative to the Tube | |
| Multistack Technology | At Least 6 Working Planes | |
| Multiple Radius Tooling | Supports Installation of Multiple Tools with Different Radii | |
| Multiple Clamping Configurations | Supported | |
| Tight Radius Bending | CLR/DIA Ratio Lower Than 0.8 | |
| Variable Radius Bending | Thrust Bending with Variable Radius | |
| Automatic Production Integration | Loading, Unloading and Automated Work Cell Integration | |
| Energy Saving | Fully Electric Drive and Pneumatic Balancing Technology | |
| Set-Up Efficiency | Technology Designed to Reduce Set-Up and Start-Up Time | |
| Scrap Reduction | CNC and Digital Drive Technology Designed to Reduce Production Scrap | |
| DESCRIPTION | ||
| The CRIPPA CA 1042E is a 20 kW fully electric CNC tube bending machine from the UP&DOWN series, equipped with 10 CNC-controlled axes and designed for high-precision right and left tube bending. The machine is capable of processing mild steel tubes up to Ø 42 × 2 mm (Ø 1.654″ × 0.079″) and stainless steel tubes up to Ø 42 × 1.3 mm (Ø 1.654″ × 0.051″). Maximum bending radius is 150 mm (5.906″), while maximum bending speed reaches 240°/sec. One of the principal features of the 1042E is the orthogonal movement of its bending head. The head can move to different lateral positions around the tube – above, below, right and left – allowing rapid changes of the working plane and helping overcome dimensional interference between the machine and the processed workpiece. This configuration enables complex tubes that would normally require additional post-processing operations to potentially be completed within a single bending cycle, improving precision and production efficiency. The machine is capable of both right-hand and left-hand bending and can be integrated with automatic loading and unloading cycles. The clamp die and pressure die operate synchronously. When the upper working plane moves forward, the lower plane moves backward, and vice versa. The CA 1042E is a multistack tube bending machine offering at least six working planes. Its substantial vertical movement allows multiple tools with different bending radii and clamping configurations to be installed on the machine. The linear movement system incorporates lubrication-free linear guides and recirculating ball carriages. High-load ball screws efficiently drive the clamp and pressure dies. A dynamic plane positioner is incorporated to help limit component damage in the event of accidental collisions by positioning the pressure-die motor to help avoid interference. All 10 axes are driven by fully electric digital motors and controlled through a Siemens SINUMERIK 840D sl CNC system. The fully electric technology is designed to provide high precision and production quality while reducing energy consumption, set-up time, start-up time and production scrap. Additional energy efficiency is provided by pneumatic balancing, which allows the use of a smaller but high-performance motor. The machine is capable of bending tubes with a CLR/DIA ratio lower than 0.8 and can perform thrust bends with variable radii. Its high production capability, wide range of possible accessories, bidirectional bending capability and ability to integrate into automated work cells make the CA 1042E particularly suitable for demanding tube manufacturing applications where productivity, flexibility and efficiency are important. Operator interaction is provided through three-dimensional graphical software displayed on a 19″ LCD touch screen. The UII (User ISO Interface) supports programming, simulation and optimisation of the tube bending process. The CRIPPA CA 1042E is also designed for integration into Smart Factory production systems. | ||